If you’ve ever ordered a forged automotive crankshaft, agricultural implement part, or heavy equipment component, you might not stop to wonder: why does that part end up fitting so perfectly into the assembly line, instead of being scrapped halfway through or failing within a month of use? As a forging part machining supplier that’s been in the game for 12 years (let’s call it “grinding parts that can’t be messed up” for short), I can tell you it all starts with picking the right machine tools. Skip that step, and you’re not just wasting material—you’re burning through client trust faster than a forge runs through billet steel. Forging Part Machining
First off, let’s get one thing straight: forging parts aren’t like the aluminum brackets you mill for smartphone cases. Forged components come out of the press hot, often with a thin, crumbly layer of scale on them, plus they’re usually made of tough stuff—alloy steel, carbon steel, sometimes even titanium for aerospace bits. That “tough stuff” doesn’t play nice with regular lathes or mills built for soft plastics or thin aluminum. So the first non-negotiable requirement is rigidity. I learned this the hard way back in 2017, when I bought a cheap used vertical mill to handle a run of 500 forged gears for a construction equipment client. By the end of the batch, we had 47 parts with wobbly tooth profiles and 12 that cracked right through the hub mid-machining. Turned out the mill’s table and spindle weren’t rigid enough to handle the constant feed of forged steel, so every cut would vibrate, skip, or bend the tool just enough to ruin the part. Now, I only run machines with thick cast-iron frames—they dampen vibration better than any steel or hybrid frame I’ve tested. Even if it means paying 20% more up front, it saves me from reworking 100 parts a week.
Next up, tool holding and spindle power. For those who don’t speak machining lingo: the spindle is the rotating part that grabs your cutting tool, and tool holding is the clamp that keeps that tool tight. Forged parts need deep cuts sometimes, right? You’re not just shaving a thousandth of an inch off a smooth surface—you’re cutting through scale, then removing excess material from a thick forged billet in one go. If your spindle doesn’t have enough horsepower, it’ll stall, snap the tool, or leave a rough surface that requires a secondary polish. A while back, we had a client in the energy sector drop off a batch of forged pump shafts that had a 2-inch-diameter section to be turned down to 1.8 inches in a single pass. Our old spindle (50 hp) couldn’t handle it, so we rented a 100 hp horizontal lathe for the job. No snags, no broken tools, and the surface finish was so smooth the client skipped the inspection polish—saved them $2k and us the headache of a rush rental. Also, tool holding: I use HSK-A100 holders now, not the old CAT holders. They grip the tool at both the shank and the face, so when you’re pushing 1,000 pounds of force through a 2-inch end mill, the tool doesn’t slip. That was another mistake I made early on—using cheap collets that wore out after 50 cuts. Now, I change tool holders every 100 cuts, no exceptions.
Then there’s thermal stability. Wait, why would a machine tool need to stay thermally stable for forging parts? Because forged parts come from forging at super high temps—up to 2,300°F—and even after they’re cooled, they can have residual stress. But more importantly, machine tools generate heat when they run: the spindle, the way the table moves, even the hydraulic system. If a machine warms up 10 degrees during an 8-hour shift, its frame expands just enough to shift the spindle by a few thousandths of an inch. For a forged part that needs to fit a gearbox with zero play, that’s the difference between a part that works and one that rattles apart in the field. I once had a job making forged tie rods for a tractor manufacturer—each rod needed a 0.002-inch tolerance on the threaded ends. We started on a machine that didn’t have thermal compensation, and by shift’s end, the threaded ends were off by 0.008 inches. The client sent a inspector that night, and we moved the run to a machine with a built-in thermal sensor that adjusts the spindle position in real time. No more tolerance issues. Thermal stability isn’t a “nice to have” for forging parts—it’s a requirement, full stop.
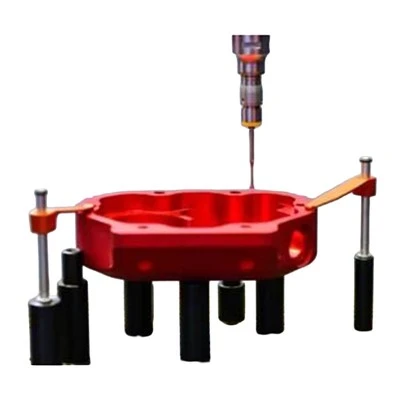
Don’t forget about the ability to handle rough stock variation. Forging isn’t like 6061 aluminum billet that comes out of a factory exactly the same size every time. Each forged part can have slight variations in shape, because the press has minor wear, or the billet’s grain isn’t perfectly uniform. So your machine tool needs to have enough rigidity and adaptive control to account for that. A lot of entry-level CNC machines only run from pre-programmed coordinates, so if a forged part is 0.1 inches wider on one side, you’ll cut too much on the thin side and not enough on the wide side. Now, all our mills and lathes have probing systems—they run a tiny cut before the main program to measure the part’s current size, then adjust the tool path automatically. Last year, we got a last-minute run of forged hammer heads for a demolition company that had 20% more shape variation than our standard stock. Without probing, we would have scrapped 30 heads out of 100. With probing, we only scrapped 2. That’s the kind of difference that keeps clients coming back instead of leaving for a competitor.
Wait, also: chip handling. Forged steel produces a TON of long, stringy chips when you machine it. If those chips get stuck between the tool and the part, they’ll scratch the surface, cause vibration, or even crack the tool mid-cut. I’ve seen machines that clog up with chips so bad the spindle overheats and burns out. So when I’m buying a new machine, the first thing I check is the chip conveyor. Does it have a high-temp chain that can handle hot chips right off the cut? Is the tank under the machine big enough to hold a full shift’s worth of chips without overflowing? We run high-pressure coolant too—like 1,000 psi—because it not only cuts down on heat, but it blasts chips away from the cutting zone fast. A lot of smaller machining shops skip the high-pressure coolant to save money, but it’s a must for forging parts. I learned that when we had a client pay us a premium for parts that had zero surface scratches—swear the last batch they got from a shop had chips left in the grooves, so they had to rework every part by hand. Now, we don’t take jobs that don’t have high-pressure coolant.
And let’s talk about tolerance. For forged parts, tolerance isn’t a “whatever works” thing. We deal with tight tolerances—sometimes ±0.001 inches—because these parts go into heavy machinery, engines, aerospace craft. If a forged jet engine turbine blade is even a hair off, it can cause the engine to fail mid-flight. So your machine tool has to have a high position accuracy and repeatability. Accuracy is how close the cut is to the programmed size; repeatability is how consistent it is cut after cut. I’ve tested machines that had great accuracy but terrible repeatability—cut part 1 perfectly, then part 50 was 0.005 inches off, just because the motor wasn’t consistent. For forging parts, repeatability is more important than accuracy, because you need every part in a run to match. So we calibrate every machine every month, and we only use machines with linear encoders instead of rotary encoders. Linear encoders measure the actual position of the table, not just the motor’s rotation, so they’re way more consistent. That’s another cost saver—if your parts are consistent, your client doesn’t have to inspect every single one, which means they’ll pay you faster and give you more work.
Now, I know what some people are thinking: “Can’t you just finish the forged part manually if the machine is bad?” Sure, you can sand down a rough surface, but you can’t fix a wobbly gear tooth or a misaligned pump shaft by hand. Those parts will fail, and when they fail, you’re on the hook for warranty work, not to mention your client’s lost revenue. That’s why I don’t cut corners on machine tools. I see other machining shops that buy cheap machines to undercut my prices, and they end up sending me their rework jobs half the time. Because when a client gets a bad batch of forged parts, they’ll ask whoever they trust to fix it, and that’s usually me.
Let’s wrap this up: the non-negotiables for machine tools when machining forging parts are, in no particular order: extreme rigidity to handle tough material and heavy cuts, enough spindle power and proper tool holding to avoid stalling or broken tools, thermal stability to keep tolerances tight over long runs, probing systems to account for forged stock variation, good chip handling and high-pressure coolant to avoid scratches and damage, and consistent repeatability to make every part identical.
If you’re a procurement manager or engineer needing reliable forging part machining, I’ve got all that and more. We’ve worked with auto, ag, energy, and even aerospace clients, and every part leaves our shop with a guarantee it’ll fit the first time. Hit me up, and we can walk through your project, talk about your tolerance needs, and make sure the machine tools we use are exactly what your parts need. No jargon, no hidden fees—just parts that work.
References
Iron Casting Machining Machining Forged Components: Key Considerations for Tooling and Machine Selection. Modern Machine Shop, 2022.
Rigidity and Vibration Control in CNC Machining of Tough Alloys. Journal of Manufacturing Processes, 2019.
Thermal Compensation Strategies for High-Precision Machining Centers. International Journal of Machine Tools and Manufacture, 2021.
Ningbo Yirui Machinery Manufacturing Co., Ltd.
As one of the most professional forging part machining manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale durable forging part machining made in China here from our factory. Customized orders are welcome.
Address: No.107, Wanzhong Village, Jishigang Town, Haishu District, Ningbo City
E-mail: James.he@yiruitek.com
WebSite: https://www.yiruime.com/
